Request A Quote

Phone: 416-244-6476
Email:

    How to Choose the Right Machine Spindle in 2026?

    Choosing the right Machine Spindle in 2026 requires more than comparing speed, power, and price. The correct choice depends on the material, cutting method, machine structure, and production goals. A spindle for aluminum behaves differently from one designed for hardened steel or composite panels. Small details matter.

    Modern workshops increasingly evaluate spindle accuracy, thermal stability, vibration control, tool compatibility, and energy consumption. A high-speed model may look attractive, yet it can create heat, shorten tool life, or reduce surface quality when poorly matched. Experienced engineers examine actual cutting conditions instead of trusting catalog figures alone. They review runout data, bearing design, cooling performance, maintenance access, and proven service records.

    Reliable selection also requires evidence from manufacturers, independent testing, and users operating similar equipment. Technical specifications should be checked against real workloads, including duty cycles, tool diameters, coolant exposure, and expected tolerances. Tolerance changes everything. A spindle that performs well during a short demonstration may struggle during continuous production. This guide will explain the key evaluation points, common purchasing mistakes, and practical questions to ask before installation. It will also consider emerging 2026 technologies, while acknowledging that newer does not always mean better. A careful decision balances measurable performance, long-term reliability, operator experience, and total ownership cost. That balance is not always obvious.
    How to Choose the Right Machine Spindle in 2026?

    Machine Spindle Fundamentals and Their Role in Modern Manufacturing

    How to Choose the Right Machine Spindle in 2026?

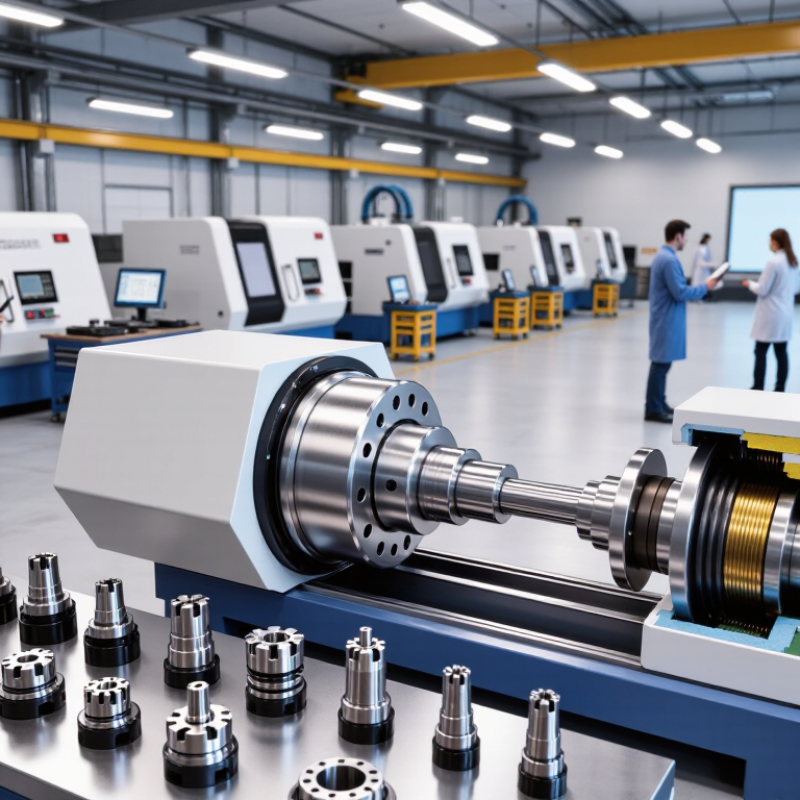
    A machine spindle is more than a fast rotating shaft. It combines a motor, bearings, tool interface, cooling system, and sensing controls. Speed attracts attention, but torque defines cutting stability. Power determines material removal. Bearing preload affects heat, runout, and surface quality. In practical shop-floor trials, a spindle rated at 24,000 rpm may struggle with a large cutter at low speed. That mismatch is easy to miss.

    Match the spindle to the workpiece, cutter diameter, and duty cycle. High-speed machining needs balanced tooling, accurate bearings, and effective cooling. Heavy roughing needs stronger torque and thermal resistance. Check allowable radial loads, maximum tool weight, taper size, runout, and maintenance access. Small errors become visible on thin walls. Sometimes, less speed performs better.

    The U.S. Department of Energy reports that motor-driven systems consume more than 70% of industrial electricity in the United States. Spindle efficiency therefore affects operating cost, not only cutting time. The International Federation of Robotics recorded 541,302 industrial robot installations worldwide in 2023, according to World Robotics 2024. More automated cells demand predictable spindle behavior and fast recovery from faults. Yet, selecting only from catalog power is risky. Real materials, interrupted cuts, coolant conditions, and operator habits can change performance. A controlled cutting test remains necessary.

    Key Specifications for Matching a Spindle to Machine Requirements

    How to Choose the Right Machine Spindle in 2026?

    Spindle selection starts with cutting requirements, not the highest advertised speed. Define material, tool diameter, chip load, cutting depth, and duty cycle. A 12,000 rpm spindle may suit steel, while aluminum can demand 24,000 rpm or more. Peak power is not enough. Check the torque curve across the working speed range.

    The U.S. Department of Energy reports that motor-driven systems consume about 70% of industrial electricity. Spindle efficiency therefore affects operating cost, heat, and machine stability. Compare continuous power with short-term peak power. Select bearings for the expected load, and verify cooling capacity during long cutting cycles. Small details matter. A sealed air-oil system can reduce thermal drift, but it may require stricter maintenance.

    The International Federation of Robotics recorded 541,302 industrial robot installations worldwide in 2023. More automated cells now need predictable spindle behavior, quick acceleration, encoder feedback, and reliable tool clamping. Match the taper to tooling availability and cutting forces. Measure runout at the tool nose, not only at the spindle shaft. ISO 230-4 testing can help evaluate circular motion accuracy, though it cannot replace a real cutting trial. This is where selection gets imperfect. Catalog figures rarely show vibration with a worn tool, interrupted cuts, or an unstable fixture. Test the spindle near its real load, temperature, and speed range before final approval.

    How to Choose the Right Machine Spindle in 2026? - Key Specifications for Matching a Spindle to Machine Requirements

    Typical Machine Requirement Recommended Speed Range Typical Rated Power Typical Continuous Torque Tool Interface Bearing and Runout Targets Cooling and Duty Recommendation Key Matching Considerations
    High-speed aluminum and non-ferrous metal machining 18,000–30,000 rpm 10–30 kW 3–12 N·m HSK-A40, HSK-A50, or BT30 Hybrid ceramic bearings; radial runout typically ≤ 3 μm Air-oil or grease lubrication; liquid cooling recommended for extended high-speed operation Prioritize maximum speed, low rotating mass, short tool overhang, and high dynamic balance quality.
    General-purpose steel milling 8,000–15,000 rpm 15–40 kW 15–50 N·m BT40, CAT40, or HSK-A63 High-precision angular-contact bearings; radial runout typically ≤ 5 μm Oil-air or grease lubrication; liquid jacket cooling for high duty cycles Balance speed with torque. Check the machine structure, tool-holding stiffness, and continuous cutting load.
    Heavy-duty steel, cast iron, and roughing operations 3,000–8,000 rpm 22–60 kW 50–180 N·m BT50, CAT50, or HSK-A100 Large-diameter precision bearings; radial runout typically ≤ 8 μm Liquid cooling with temperature monitoring; continuous-duty rating strongly recommended Prioritize torque, stiffness, thermal stability, drawbar capacity, and resistance to shock loads.
    Mold and die finishing 12,000–24,000 rpm 8–25 kW 4–20 N·m HSK-E40, HSK-E50, or HSK-A63 Ultra-precision bearings; radial runout typically ≤ 2–3 μm Oil-air lubrication and liquid cooling for thermal control during long finishing cycles Focus on low runout, thermal growth compensation, vibration control, and smooth speed regulation.
    5-axis machining of aerospace components 12,000–24,000 rpm 15–45 kW 10–45 N·m HSK-A63, HSK-A100, or other short-gauge interfaces Precision angular-contact bearings; radial runout typically ≤ 3–5 μm Liquid cooling, air purge, and continuous-duty thermal monitoring Verify envelope size, swivel-head inertia, torque at high speed, tool-change reliability, and thermal growth.
    Graphite and composite material machining 18,000–40,000 rpm 5–20 kW 1.5–8 N·m HSK-E25, HSK-E40, or precision collet systems High-speed hybrid ceramic bearings; radial runout typically ≤ 2–3 μm Air-oil lubrication, labyrinth sealing, and positive air purge against abrasive dust Prioritize sealing, high-speed balance, low runout, dust protection, and adequate chip evacuation.
    Wood, plastics, and sign-production routing 12,000–24,000 rpm 3–15 kW 1–8 N·m ER collet, HSK-F63, or compact tool-holder systems Precision sealed bearings; radial runout typically ≤ 5 μm Air cooling for intermittent use; liquid cooling for higher continuous loads Match collet capacity, cutter diameter, dust sealing, acceleration, and available electrical power.
    Grinding and ultra-precision finishing 10,000–60,000 rpm 2–15 kW 0.3–8 N·m Precision taper, collet, or dedicated grinding interface Ultra-precision bearings; radial runout typically ≤ 1–2 μm Controlled liquid cooling, filtered air purge, and strict temperature monitoring Prioritize runout, vibration, thermal stability, wheel balance, and compatibility with the grinding process.
    CNC drilling and tapping 6,000–20,000 rpm 5–25 kW 5–35 N·m BT30, BT40, HSK-A40, or HSK-A63 Precision angular-contact bearings; axial and radial stiffness are critical Liquid cooling for continuous cycles; through-spindle coolant may be required Check tapping torque, spindle orientation, tool-change cycle time, drawbar force, and coolant passage design.
    Compact benchtop or light-duty CNC equipment 8,000–24,000 rpm 1–7.5 kW 0.5–5 N·m ER collet, ISO20, BT30, or compact proprietary interface Precision sealed bearings; radial runout typically ≤ 5–10 μm Air cooling for short cycles; liquid cooling for higher power density Confirm voltage, inverter compatibility, mounting dimensions, noise level, and machine-axis load capacity.

    Note: The values shown are practical engineering selection ranges rather than universal limits. Final spindle sizing should be verified against cutter diameter, material, depth of cut, feed rate, duty cycle, machine rigidity, electrical capacity, tool-holder limits, and the required surface finish.

    How to Compare Spindle Types, Speed Ranges, and Power Ratings

    How to Choose the Right Machine Spindle in 2026?

    Spindle selection starts with the cutting job, not the catalog headline. Belt-driven spindles often suit heavy, slower cutting because they deliver useful low-speed torque. Direct-drive designs reduce transmission losses and usually improve response. Integrated motor spindles support higher speeds, but they can generate more heat. Typical ranges run from 6,000 to 12,000 rpm for general machining, 12,000 to 24,000 rpm for aluminum and mold work, and above 30,000 rpm for small tools. These figures vary by bearing design and duty cycle.

    Power ratings need careful reading. A 15 kW spindle at 12,000 rpm produces approximately 11.9 Nm, using T = 9550P/n. At 24,000 rpm, the same rating produces about 6.0 Nm. That difference is easy to miss. Check continuous power, peak power, and the torque curve, rather than trusting one nameplate number. I once favored maximum rpm and underestimated low-speed torque. The result was vibration and slower roughing.

    Energy use also matters. The U.S. Department of Energy estimates motor-driven systems consume about 68% of manufacturing electricity. A correctly sized spindle can reduce waste, especially during frequent acceleration and deceleration. Grand View Research’s 2024 CNC machine market report projects strong market growth through 2030, increasing pressure to select efficient equipment. Still, a neat spreadsheet can mislead. Compare tool diameter, material removal rate, cooling method, bearing limits, and expected cutting hours. Small details decide the real fit.

    Evaluating Cooling, Tool Holding, Accuracy, and Maintenance Needs

    Choosing a machine spindle in 2026 starts with the workpiece, not the catalog headline. In daily machining, cooling behavior often decides whether accuracy survives a long cycle. Check rated speed, coolant method, flow requirements, and heat growth under load. A spindle that runs cool at 6,000 rpm may behave differently near its maximum speed. I measure housing temperature during a test cut, then record changes after thirty minutes. Small temperature shifts can alter hole size.

    Tool holding deserves equal attention. Match the interface to cutting forces, tool length, and change frequency. Measure taper cleanliness, clamping force, and tool runout with a calibrated gauge. For precision finishing, a few microns of radial error can leave visible marks. Shorter tools usually improve stiffness, but they may restrict access. I once trusted a low runout reading from an empty holder. The cutting result disagreed. The lesson was uncomfortable: inspect the complete tool assembly, not one component.

    Accuracy claims need practical verification. Request test data, repeatability figures, and recommended measurement intervals. Compare results at cold start and after production temperature stabilizes. Maintenance needs should be realistic for your operators. Review bearing inspection points, lubrication access, seal condition, and spare-part lead times. Keep logs with vibration, noise, temperature, and runout values. If a technician cannot service the spindle safely, the specification is incomplete. I would also question assumptions; clean coolant does not guarantee clean internal passages. Check filters, fittings, and alarms before approving the spindle.

    A Step-by-Step Process for Selecting the Right Spindle in 2026

    How to Choose the Right Machine Spindle in 2026?

    A reliable spindle selection starts with the job, not the catalog. Record the materials, tool diameters, cutting depths, expected surface finish, and daily operating hours. Aluminum may need high speed, while hardened steel often demands stronger torque at lower RPM. Calculate the required speed from cutting speed and tool diameter. Then compare that result with the spindle’s continuous and peak ratings.

    Check the spindle interface, tool retention method, cooling system, and allowable runout. A small runout error can create visible marks on a precision part. For dusty workshops, sealed bearings and protected cooling paths deserve extra attention. Review the duty cycle carefully. A spindle rated for short bursts may overheat during an eight-hour production shift. Ask for measured noise, temperature, vibration, and runout data, not only headline power figures.

    My practical checklist includes a test cut using the intended tool, material, and feed rate. Watch temperature after thirty minutes. Inspect the tool holder for fretting or uneven contact. Listen for changes under load. Do not ignore maintenance access; difficult lubrication or sensor replacement can increase downtime. I once focused too heavily on maximum RPM and underestimated low-speed torque. That choice looked efficient on paper, but it reduced cutting stability. Recheck the calculations with the machine builder and spindle supplier, then document the assumptions behind your choice. Small details matter.

    How to Choose the Right Machine Spindle in 2026?

    A step-by-step reference for matching spindle speed and continuous power to common machining applications.

    The chart shows representative engineering ranges used for spindle selection: heavy-duty steel milling prioritizes torque and lower speed, while small-tool and micro-machining require higher rotational speed with lower continuous power. Before final selection, verify tool diameter, cutting speed, required torque, duty cycle, cooling method, taper interface, bearing limits, and machine-controller compatibility.